Sample No. 0015
CPO Testing Needs Optical Design-for-Test as Connector Choices Evolve
CPO test is scaling toward high-volume production, but optical alignment, thermal demands and unsettled connector designs complicate the path.
Co-packaged optics is pushing test equipment into a new production regime: optical measurements must move from lab setups to automated, repeatable processes that can handle high volumes. The industry is still choosing connectors and laser sources, while data centers begin building around early generations of the technology. That leaves test manufacturers preparing for requirements that may shift before designs settle.
The challenge isn’t simply adding optical instruments to an existing test cell. Teams need reliable ways to align fibers and connectors at wafer, package and optical engine stages, then automate those connections and manage the resulting measurements at production scale. Without design-for-test features built into photonic devices, much of the work remains slow and component by component.
Experts at the table: Semiconductor Engineering spoke with Matt Griffin, senior product manager for optoelectronics test at Teradyne; Ira Leventhal, vice president of research and venture at Advantest America; Dave Armstrong, fellow at ISE Labs, a subsidiary of ASE Group; and Kazuo Yamaguchi, silicon photonics researcher and engineer at Keysight Technologies.
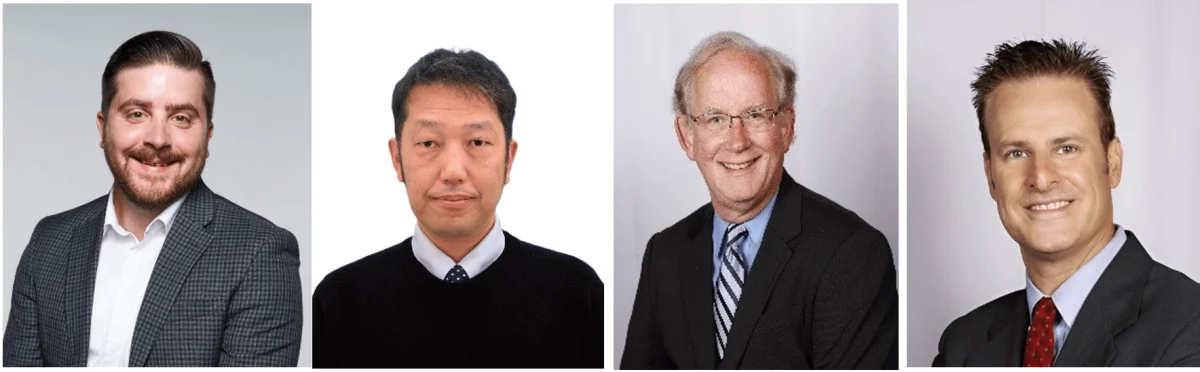
Fig. 1: (L-R): Teradyne’s Griffin; Keysight’s Yamaguchi; ISE Labs’ Armstrong; Advantest’s Leventhal.
Lab methods don’t scale by themselves
Optical transceivers have been tested for years, but co-packaged optics raises the demands on manufacturing. A characterization lab can rely on rack-mounted instruments and custom alignment equipment. A production floor needs many test cells, repeatable connections, automation, analysis software and test programs that can keep pace with throughput.
Griffin identifies two major changes: optical instrumentation suited to wafer, optical engine and package testing, and automation for making the optical connection. Depending on the device and test stage, that may mean aligning a fiber at wafer level or connecting to a receptacle on a package or optical engine. Bringing lab equipment into a production cell doesn’t solve the problem on its own; the alignment process and surrounding workflow must work reliably at volume.
Leventhal sees this as another step in the expansion of automated test equipment. Electronics test grew from digital testing to cover increasingly integrated digital, analog, mixed-signal, radio-frequency and millimeter-wave functions. Photonics extends that progression, but the ecosystem for optical test remains less mature. Engineers also need to account for optical measurements such as polarization extinction ratio, which require knowledge beyond familiar electrical test methods.
The gap is especially visible in design-for-test. Armstrong compares the current situation to logic devices before scan test became common. Without optical test structures or other built-in ways to observe device behavior, manufacturers may need to measure individual waveguides, resonators, modulators and photodiodes. That approach is laborious and difficult to scale. Pseudo-random binary sequence methods are being tried in some cases, but they don’t amount to broadly adopted optical design-for-test.
There’s also a skills gap between optical and electrical engineering teams. Production test brings both disciplines together, yet practitioners may not share methods, terminology or assumptions. Armstrong argues that teams need a common technical foundation and compatible standards if they’re to decide what to measure and how to interpret the results.
Alignment and calibration carry production risk
Optical connections are sensitive to small positional errors. Yamaguchi says an optical probe card could help, but creating one is difficult: the mechanical interface must work without contact in the usual way, and the optical system needs calibration so measurements remain reliable and traceable.
Multi-channel fiber array units (FAUs) can vary from one unit to another and from channel to channel. As a result, a measurement taken on one waveguide channel may not match the same measurement on another. Small differences in pitch or x-and-y position can shift optical alignment and affect readings more than a comparable offset in electrical probing.
Physical variation doesn’t stop at the connector. Large packages can warp, shifting connection points from their expected positions. Leventhal warns that a connector meeting a warped package may miss its target or shear off. High power adds another constraint: Griffin says customers are considering requirements of 1 to 8 kW for the central compute die and 10 to 30 W for each optical engine. Managing heat under those conditions is a key part of test design.
Test coverage is spread across the flow
Armstrong describes a possible sequence of five test insertions: photonics integrated circuit testing at wafer level; wafer-level optical engine testing; die-level optical engine testing; module testing; and system-level testing. A wafer-level burn-in step may sit between the first two. He describes that stability bake as particularly important for lasers, helping screen early failures.
Photonics integrated circuit testing is already widespread, though some experienced practitioners expect it may become less necessary as manufacturing matures. The optical engine stages are newer and drawing much of the current effort. Armstrong says hyperscalers appear to regard the second, third and fourth insertions as necessary, extending their established practice of testing high-power, heterogeneous packages with automated equipment.
There’s no single test point that every customer treats as the priority. Griffin says the most important insertion has varied with each customer and market segment. His view is that test systems should support coverage across the flow so manufacturers can adjust where they test as they learn which steps best protect yield and production efficiency.
One important checkpoint comes before the optical engine is attached to a high-performance compute device. A defective, lower-cost engine discovered after assembly could put the yield of a much more valuable package at risk. Later, manufacturers may want a full functional test of the assembled CPO module. Customers differ on whether to run that test on automated equipment, at system level, or in both places. The module may require optical connections through 4 to 32 connectors, adding setup and thermal demands.
Yamaguchi notes that many measurement parameters and compliance metrics already come from optical transceiver practice. The key change is where in the manufacturing flow those measurements happen and how early. Industry standards are being developed alongside discussions about CPO and near-packaged optics test, so manufacturing plans and test definitions are evolving together.
Leventhal expects some steps to disappear as packaging and manufacturing processes improve. Others may remain fundamental, while added design-for-test features could provide needed information through a more efficient route. In the meantime, less mature processes may require more burn-in stages. The test flow is therefore likely to change as engineers separate temporary process checks from measurements that continue to show whether the system works as intended.
Connectors remain an open choice
Test providers have to accommodate whichever connector designs customers select, and those options have different trade-offs. Some designs prioritize connection repeatability and reliability; others favor optical performance. Compatibility with different FAUs matters too. If suppliers can’t meet demand and manufacturers qualify another FAU source that uses a different connector, test equipment and production setup may become harder to standardize.
Griffin expects a small group of customers to reach volume and begin shaping connector choices over the next one to two years. Armstrong describes the situation as unsettled: manufacturers are discussing two-row fiber arrays and FAUs containing hundreds of fibers, even as earlier alignment challenges remain unresolved.
Cleaning is another production detail with direct consequences for optical measurement. Dust can interfere with the connector and FAU, and each cleaning cycle may introduce more particles. Armstrong says automated cleaning will be important as these connections move into production.
The near-term task is to build test cells that can absorb connector variation, control alignment and heat, and collect useful measurements without relying on slow component-by-component inspection. As connector designs and manufacturing volumes settle, the biggest gain may come from photonic devices designed to expose test information directly. Without that change, adding capacity will be harder than adding instruments.
The post CPO Testing Faces A Moving Target Problem appeared first on Semiconductor Engineering.