Sample No. 0221
Co-Packaged Optics Testing: Failure Diagnosis, Cost and Scale
CPO raises the cost of a missed defect. Better fault isolation, earlier screening and coordination across engineering teams will shape its path to production.
Co-packaged optics (CPO) changes the economics of test because an optical failure can put a far more expensive chip at risk. That makes early screening and clear fault diagnosis central to scaling production. The challenge reaches beyond test equipment: teams need to agree on measurement boundaries, design in ways to isolate components, and weigh optical performance against the serviceability and throughput demands of manufacturing.
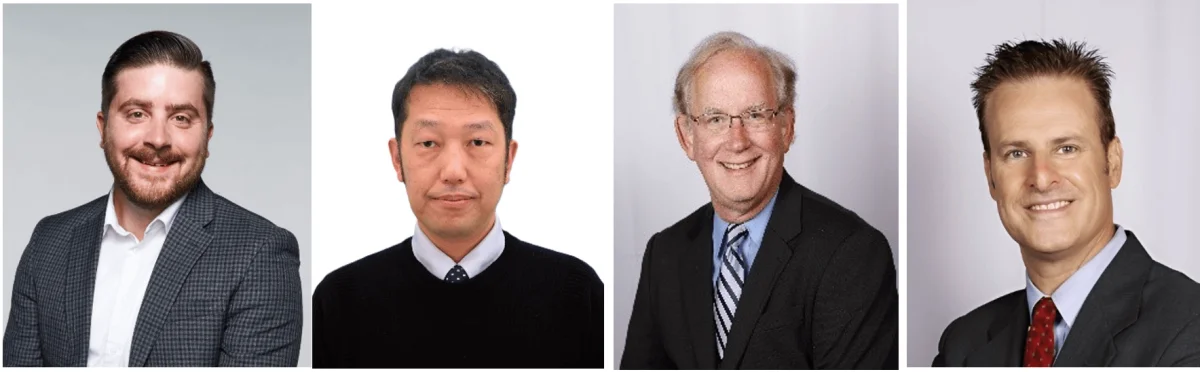
Those themes emerged in a discussion with Matt Griffin, senior product manager for optoelectronics test at Teradyne; Ira Leventhal, vice president of research and venture at Advantest America; Dave Armstrong, fellow at ISE Labs, a subsidiary of ASE Group; and Kazuo Yamaguchi, silicon photonics researcher and engineer at Keysight Technologies. Their discussion focused on failure analysis, test costs and the work needed to bring CPO into high-volume manufacturing.
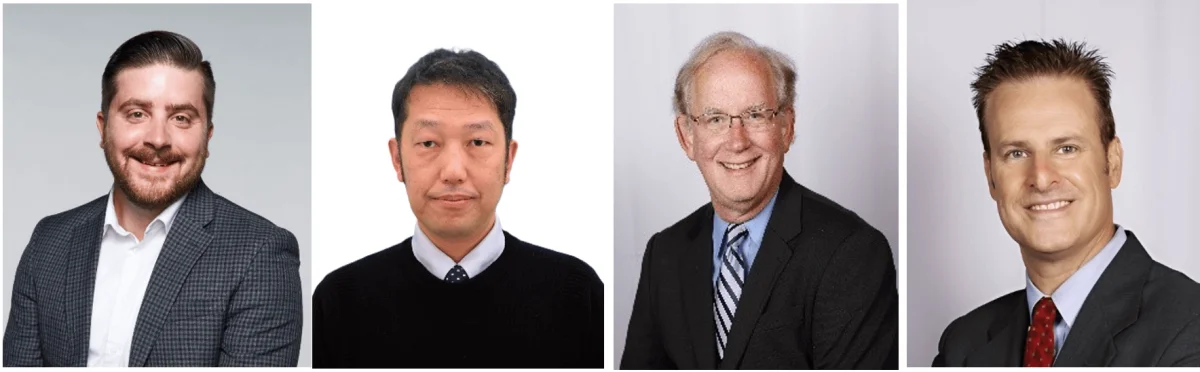
Fig. 1: (L-R): Teradyne’s Griffin; Keysight’s Yamaguchi; ISE Labs’ Armstrong; Advantest’s Leventhal
Fault isolation starts with measurement boundaries
To trace a failure, engineers first need to know exactly where each measurement begins and ends. Yamaguchi described setting reference planes at physical, electrical and optical interfaces. Depending on the test, a boundary might sit at a die pad, package ball, connector or fiber interface. Measurements taken at different stages must use aligned boundaries; otherwise, changes in test setup can look like changes in the device.
Everything between those planes can affect the result. Probes, sockets, traces, connectors and patch cords may need to be de-embedded, or accounted for separately, so their effects aren’t mistaken for a device fault. When testing one part of an optical system, engineers can substitute a neighboring component with a characterized reference. For example, a known-good laser source can stand in for the laser while the optical engine is evaluated.
That reference raises a practical question: how much of the source should test treat as a known-good input? Leventhal argued that the purpose is to test the component under evaluation, not turn every test into a laser qualification exercise. He compared the laser to a device power supply in an electrical test setup: the test assumes it works as intended. Customers may prefer the laser used in normal operation, but Leventhal noted that this source isn’t an automated test instrument. The test approach will need to account for that distinction.
Griffin pointed to monitor photodiodes and optical taps as ways to see what is happening inside a signal path. A tap can route light to characterization equipment or let a team monitor power during loopback or mission-mode testing. That visibility is useful when teams don’t plan to run a full characterization on every unit. But a basic functional check can show that a link failed without explaining why. Access to the loopback path can give engineers another place to investigate.
Integration makes failures harder to untangle
The labels near-packaged optics (NPO) and CPO don’t have a single, consistent definition, Griffin cautioned. Both involve aligning multiple optical connectors and delivering power to the device. One possible distinction is whether the optical engine can be detached. That may make a failure easier to address, but reworking and reattaching an engine later in the process can be difficult. Customers may still want each engine to be known-good before integration.
CPO places more components together in the package, which increases the need to separate their contributions during diagnosis. Leventhal said design for test (DFT) can help by exposing information about individual components and connecting those results to failures observed in the assembled package. The goal is to avoid treating the package as an opaque unit when one element underperforms.
The electrical architecture also matters. Yamaguchi described retimed NPO, where the optical engine has its own digital signal processor (DSP), as easier to test independently. It can be checked much like a pluggable optical module, making a fault simpler to locate. Linear-drive NPO removes that DSP: the host ASIC’s SerDes drives the optics through linear drivers and transimpedance amplifiers (TIAs). Electrical and optical components then share one signal path, so a bad link is harder to attribute to either side. In that respect, its test challenge resembles CPO.
Thermal behavior adds another layer. Armstrong said CPO’s electrical signals can’t travel as far, while NPO may permit greater electrical reach. That reach still needs to be managed, and heat from the optical components is a significant concern. The test setup and package design therefore have to account for both signal behavior and the thermal load.
The cost of a missed defect changes the test budget
When an optical engine sits beside an ASIC or GPU costing tens of thousands of dollars, the economics of test shift. Leventhal cited GPUs and ASICs priced at $40,000 or $50,000 as examples: a comparatively inexpensive optical component must not cause one of those devices to be scrapped. Test spending has traditionally been considered in relation to chip manufacturing cost. In this setting, spending more to screen components early can make sense if it protects the assembled device.
Yamaguchi sees the same shift in the rising value of the device, the potential scrap cost, and the complexity of both test and packaging. That makes additional wafer or optical-engine testing easier to justify. Screening before assembly can catch problems before they become costly package failures, moving some of the test effort earlier in the manufacturing flow.
Griffin added that data center operators want to deploy AI accelerators and network switches at scale. The optical engine’s value can’t be judged in isolation from the package and system function it enables. In his account, optics can reduce power and support disaggregated computing architectures. That makes reliable testing part of the effort to deliver these systems efficiently.
Armstrong said surveys conducted by IPSR indicate that testing an optical component is approaching the cost of manufacturing it, and that rising complexity could push test costs higher still. The industry may therefore need to accept a larger test budget to secure quality components and known-good die. Test economics will also depend on how the cost is distributed among the companies and teams involved.
Production needs an ecosystem, not just a test cell
Leventhal said the current challenge is scaling CPO into high-volume manufacturing, rather than proving that the technology works. He cited reliability data presented by Meta earlier in the year as evidence that CPO can be reliable. The next phase, in his view, will rely on added screening, burn-in, more test insertions and tighter engineering controls while the manufacturing ecosystem matures.
NPO can help build experience along the way because it presents a lower hurdle to deployment. Lessons from NPO may inform CPO manufacturing, but Leventhal warned that the transition won’t be automatic. Standards and multi-source agreements (MSAs) can help companies align platforms and define manufacturing requirements. Yamaguchi said this work doesn’t alter measurement science; it helps partners agree on criteria, such as the optical power to transmit and the bias to apply.
Inside each company, Griffin sees a coordination challenge between photonics specialists and semiconductor test teams. Photonics groups may know how to characterize devices, while high-volume test teams focus on uptime, software and service support, and deploying many test cells. Choices made for flexibility, modularity or easier servicing can affect optical performance. For instance, a connector selected to support flexibility or more channels may deliver less optical power at the device under test, with consequences for system design.
Those tradeoffs need input from designers and manufacturing teams who understand the device. Test costs are already approaching manufacturing costs for optical components, and the value of the surrounding chip raises the cost of getting the decision wrong. As production ramps, the practical work is to connect component level diagnosis, package level test and factory requirements. Better visibility into individual components—and agreement on how to measure them—will determine how efficiently CPO moves from working systems to repeatable production.
Read parts one and two of the discussion:
CPO Testing Faces A Moving Target Problem
Test vendors are adapting to changing connector architectures and extreme alignment tolerances as co-packaged optics heads toward mainstream.
Scaling CPO Testing Beyond A Single Die
Fiber alignment, connector durability, and simultaneous optical and electrical testing pose challenges for high-volume manufacturing.
The post Bringing Down Test Costs For Co-Packaged Optics appeared first on Semiconductor Engineering.